The counter-intuitive part of a packed ice maintenance programme is that a calendar schedule tells you least when you need it most. An edge on a route that sees a handful of freeze-thaw cycles in a mild month loses almost nothing, and the same edge in a hard month can lose more than a whole season’s worth of material in a fortnight. What actually removes material is the number of events the edge has worked, and that is the number the inspection interval should follow.
This is a verification programme rather than a maintenance schedule. It sets out what interval to use and why, what to measure at each check, the thresholds that trigger an action, how rotation fits in, and the records that turn a season of measurements into a decision about next year’s specification.
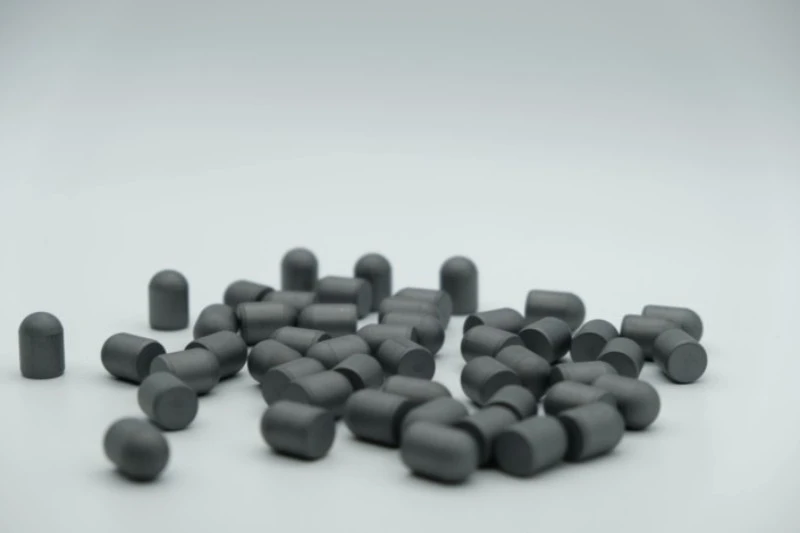
Why the interval is set by events, not by the calendar
Wear on a cutting edge accumulates with work, and on a packed ice route the work arrives in bursts. A fortnight of mild weather with a few passes a day removes far less than a single week of repeated freeze-thaw cycles, and a monthly inspection schedule will catch both at the same point in the calendar having done very different amounts of damage.
Anchoring the interval to events also makes measurements comparable. A reading taken after a set number of ice-control events can be compared with a reading taken at the same point on another route, or on the same route in another season. A reading taken at the end of a calendar month cannot, which is why so many fleets hold years of measurements that they have never been able to use.
The event count is already recorded for other reasons on most routes, which means the change costs nothing beyond moving the inspection trigger to the record the fleet already keeps.
What a season of packed ice work does to an inspection plan
A packed ice edge changes in two ways that a general fleet inspection does not anticipate. The first is the rate: material loss accelerates once the edge begins to ride rather than cut, because the contact changes from cutting to sliding and the edge is then being worked against a surface it cannot affect.
The second is the geometry. As the contact face wears, the way the edge meets the pavement changes, and an edge that was cutting in December can be riding by February with nothing having broken. Neither change is visible from a walk-around, and both are why the measurement rather than the visual check is the part that matters.
Packed ice edge inspection: interval by event count
Count events, not weeks.
The workable arrangement is two triggers rather than one. The first is a routine check after a set number of ice-control events, chosen from the fleet’s own history so that it lands between the point where wear becomes measurable and the point where it changes the cutting behaviour.
The second is a mid-season check at a fixed point in the calendar, which catches the routes whose event counts have run ahead of the fleet average.
Where a fleet has no event history to work from, the first season is used to establish it: measure at the start, at the mid-season point and at the end, and record the event count alongside each reading. Even three readings across a season are enough to set the routine for the next one.
What to measure at each check
The sequence below is short enough to run in a workshop bay and consistent enough to compare across a season.
- Measure insert or contact height at several positions along the working width, not only at the centre.
- Record which positions are lowest, so the pattern can be compared with the route’s polished sections.
- Inspect the seat or joint at the worst position, looking for movement, fretting or filler left behind.
- Check the mounting line against a straight edge, since a bowed body changes the load along the whole edge.
- Record the event count at the time of measurement, so the reading has a denominator.
The second step is what turns a set of numbers into a diagnosis. Height alone says the edge wore; the position along the width says whether the cause is the surface, the fitment or the machine. What the different patterns mean is set out on the wear pattern page.
Insert condition thresholds
The thresholds below convert a measurement into an action, which is what stops a mid-season check from becoming a note in a file.
| Condition | What it means | Action |
|---|---|---|
| Even loss along the width, within the expected range | Specification and route agree | Record and continue; do not change anything |
| Loss concentrated in bands matching the route | The edge is riding the polished sections | Check angle and down pressure before changing parts |
| Loss concentrated at the ends | Impact at transitions or a mounting issue | Check the mounting line and the end support |
| Individual inserts standing proud | A partial replacement has left a mixed row | Replace the row rather than the outlier |
| Movement or fretting at a seat | The insert is loose before it is lost | Take the edge out of service and inspect the seat |
The fifth row is the only one that takes an edge off the machine immediately. Movement at a seat is a leading indicator of loss rather than a symptom, and the cost of catching it in the workshop is a fraction of the cost of catching it on a route.
Rotating to extend service life
Rotation pays where the wear is uneven along the working width, and does nothing where it is not. The decision is therefore made from the measurement rather than from a rule: a pattern with clear bands or a concentration at one end can be moved to a less heavily loaded position, and a pattern that is uniform has nothing to move.
Two practical conditions apply. The machine has to allow the edge to be repositioned without changing the fitment, which rules out edges that are keyed to a particular position. And the rotation has to be recorded, otherwise the next inspection cannot distinguish a pattern produced by the route from one produced by moving the edge between positions. Rotation practice for wear parts of this kind fits inside the wider measurement routine described on the blade wear measurement page.
Documenting wear for warranty
Wear records serve two purposes, and only one of them is planning. The planning purpose is the specification decision at the end of the season; the other is the ability to support a claim if a lot fails early.
For that second purpose, three entries matter more than the rest: the batch reference of the inserts fitted, the event count and measurement at the start, and the measurement at removal with the wear pattern noted. A claim is difficult to argue without the baseline, because there is no way to show that the edge started sound. Where a supplier issues lot documentation, keeping it with the measurement record is what makes the two usable together.
Trigger points for change-out
Change-out should follow a measurement rather than a schedule, and the sequence below sets out how the decision is reached.
- Compare the current contact height with the minimum the design allows.
- Check whether the edge still cuts on the bonded sections, rather than only measuring height.
- Check for movement at any seat or joint, which is a change-out trigger on its own.
- Check whether the wear pattern has changed since the previous reading, which indicates the route or the machine has changed.
- Record the reason for the change-out, so the next season’s specification has something to work from.
The fifth step is the one that compounds over several seasons. A fleet that records why each set of inserts was changed eventually has a distribution rather than a set of individual judgements, and that distribution is the evidence behind a specification change.
Spares and tooling to hold
Three items keep a programme running through a hard month, and a fleet that is short of any of them loses more time than the parts cost.
- A full insert row rather than individual inserts, since a mixed-height row fails early.
- The measurement instrument used in the inspection, kept with the edge records rather than in general tooling.
- Fixing hardware in the pattern the fleet runs, because a change-out that stalls on a missing fastener costs a route.
The second item looks trivial and is not. Where measurements are taken with whatever instrument is to hand, the readings differ by more than the wear being measured, and the record loses the comparability that makes it worth keeping.
Building the record into the seasonal routine
The programme survives on two fixed points in the season and one habit in between.
- Measure every edge at fitment and record the event count as zero.
- Run the routine check at the chosen event interval, recording the count with the measurement.
- Run the mid-season check on the routes whose event counts have run ahead.
- Measure every edge at removal, noting the wear pattern and the reason for removal.
Four points in a season produce a record that supports a specification review, a warranty claim and a route comparison, for the cost of a few minutes per edge. Test methods behind the material values involved are published by ASTM International and ISO, and fleet-level maintenance practice by the Snow and Ice Management Association.
SENTHAI manufactures packed ice carbide kits, inserts and cutting edges in Rayong, Thailand, and issues each lot with the reference that ties it to its production record, which is what a warranty claim is built on. Research on winter maintenance performance is published by the Transportation Research Board, network guidance by the Federal Highway Administration, and edges that need their inspection record reviewed can be raised through the contact page. How the surfaces a route presents drive the pattern being measured is described on the packed ice tactics page.
FAQ
How often should a packed ice edge be inspected?
Base the interval on the number of ice-control events the edge has worked rather than on elapsed time, because that is what removes material. A check after a set number of events, plus one mid-season, keeps the measurements comparable between routes and between seasons.
What should be measured at each inspection?
Contact or insert height at several positions along the working width, the condition of the seat or joint at the worst position, and the straightness of the mounting line. Those three together show whether the edge is wearing evenly, whether it is still cutting, and whether the body has moved.
Does rotating an ice edge actually extend its life?
Where the wear is uneven along the working width, yes, because it moves the heavily loaded positions away from the sections that are wearing fastest. Where the wear is already uniform, rotation changes nothing and the same effort is better spent on the inspection record.
Send the event counts, the height measurements and the positions that wore first. The SENTHAI engineering desk will confirm whether the pattern points to the specification, the fitment or the route.
This article is one step in the Packed Ice Edge Guide, which explains why a standard edge skates across hardpack and how to set one up so it bites.