Packed ice does not wear a plow edge down so much as teach it to stop cutting. The blade rides the surface instead of biting into it, and riding produces a wear pattern that is different in kind from ordinary abrasion: material is lost along the contact face in a flat band, the geometry that made the edge cut disappears, and the blade goes on damaging itself on a surface it can no longer affect.
This diagnostic works backwards from the damage to the cause. It covers why a polished layer forms, what riding does to the edge, how heat and impact contribute, where salt and chemicals fit in, and the evidence to collect so the conclusion rests on measurement rather than on a description.
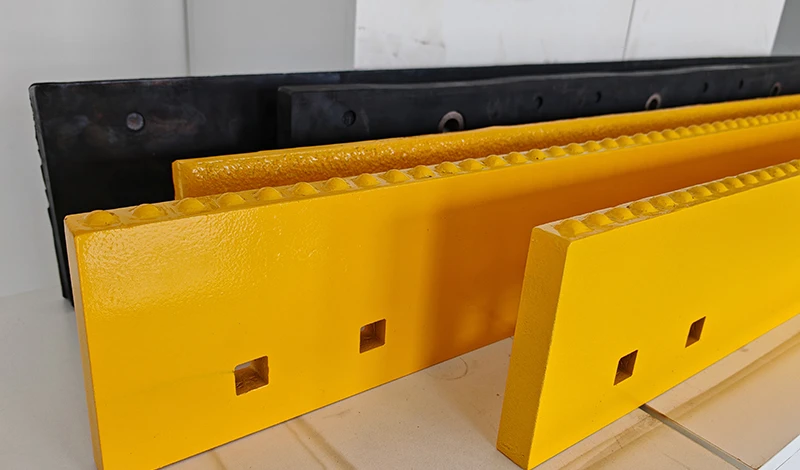
What starts the damage
The damage does not start with an impact, and that is why it is so often misread. It starts with a load that is spread too thinly to do any cutting, but is still enough to slide a steel edge across a hard surface for hours at a time.
That condition is specific to a bonded layer. On loose snow the same load clears material effectively, because the material yields. On a polished surface the material does not yield, and the energy that would have gone into moving snow goes into sliding contact instead. The edge is then being worked against something it cannot cut, in a state where the operator has no feedback that anything is wrong: the blade is down, the surface looks white, and the route takes the same time it always took.
What follows from that is a damage pattern that grows gradually and is invisible at any single inspection. The wear flat, the change in the cutting angle and the eventual loss of the ability to cut any material at all accumulate over weeks rather than hours.
What a polished layer looks like on a route
Operationally, a polished layer is easy to recognise and easy to underestimate. It appears as a white or grey sheen on the pavement, it has a hard, almost waxy feel underfoot, and it does not respond to a scraper the way drifted snow does.
Its distribution matters as much as its presence. It builds first and most heavily in the wheel tracks, because that is where traffic compresses and polishes. It forms earliest on shaded sections that do not see sun, at intersections and on inclines where vehicles stop and start through a freeze, and on sections that have been treated and then refrozen rather than plowed while soft.
The distribution explains a wear pattern that otherwise looks arbitrary: a blade wearing hardest in the middle of its width and least at the ends is following the wheel tracks rather than a defect in the edge, and the same band of damage will appear season after season until something about the surface treatment changes.
Packed ice plow blade damage: riding versus cutting behaviour
Riding damages an edge more than cutting does.
In a cutting condition, the insert or edge engages the material, load is concentrated at a small contact, and the material fails in front of the tool. In a riding condition, the same load is distributed across the whole contact face as sliding friction, with no material failure to absorb it.
The energy goes into the edge and the surface, and the edge loses material along the contact face while the surface is polished a little smoother for the next pass.
The two conditions also differ in the feedback they give the operator. Cutting produces a visible windrow and a change in the sound of the blade working. Riding produces neither, which is why a route can be worked hourly and still be in the same condition at the end of the shift. The geometry that turns one into the other is set out on the packed ice kit page.
How polished ice layers form
A polished layer is the product of repeated passes rather than a single event. The high points on a rough icy surface are removed by traffic and by plowing, and what remains is a plane that is smoother and harder than the material it came from.
Two mechanisms do the polishing. Mechanical action, where tyres and blades shear the high points off and compact what is left. And thermal action, where a partial melt at the surface refreezes into a denser layer than the original snow. Where both operate in the same place, the result is the dense, glassy surface that a scraper rides, and it is most developed exactly where traffic is heaviest and the freeze-thaw cycle is most frequent.
Heat build-up at the edge
Sliding contact generates heat, and on ice that heat has a self-reinforcing effect. A sliding steel edge can produce a thin melt film at the contact, which lowers friction and lets the edge glide further, and the film refreezes behind the blade into a smoother surface than the one in front of it.
The effect is small at any one pass and cumulative over a season. Its practical significance is that it gives a second reason for an edge to stop cutting: not only is the material harder, but the contact condition has changed to make sliding the easier outcome. It is also a reason for the wear pattern to be concentrated where the blade runs at the highest speed and the longest contact, since both raise the energy going into the contact.
Accelerated wear flat formation
A wear flat is the visible result of the riding condition, and reading it correctly distinguishes a surface problem from a fitment problem. The table below sets out the forms it takes and what each one indicates.
| Form of wear | What it looks like | What it indicates |
|---|---|---|
| Uniform flat along the width | Contact face polished and shortened evenly | The blade has been riding a polished layer across its whole width |
| Flat concentrated in wheel-track bands | Uneven loss in two bands, sound material between them | The route polishes hardest where traffic compresses |
| Flat with a rolled leading edge | Material pushed back rather than removed | Contact pressure far below what the surface requires |
| Flat plus chipping at the ends | Smooth face with chipped corners at the outer positions | Riding across the width with impact events at the transitions |
The third row is worth recognising early, because the deformation is a sign that the edge is being worked in a condition it cannot influence rather than a sign that the material is unsuitable. A measurement of the contact face against the drawing is enough to record it objectively.
Edge damage from bouncing
Riding produces a second failure mode that is easier to see and harder to attribute. Where an edge rides across a polished surface, it also rides across the depressions in it: pavement joints, utility cuts and the lip of a patched section. The blade is unsupported over those gaps, and the load it was carrying is released and reapplied in a short distance.
The result is impact damage at the positions that cross the gaps most often, which in practice means the same few places along the route and often the same positions along the edge. That pattern is frequently read as a fitment problem, and correcting the fitment does not resolve it, because the cause is the surface the edge is riding rather than the way it is mounted.
Salt and chemical interaction
Treatment chemicals change the material the edge meets more than they change the edge itself, and they do it in two directions. By lowering the freezing point, salt produces repeated partial melting and refreezing, which is one of the mechanisms that builds a dense polished layer rather than removing it. And the wet, chloride-rich environment around the blade attacks the steel side of the assembly, which is a separate problem from wear.
Keeping those two effects apart matters when the damage is being diagnosed. A blade with a wear flat and corrosion along its joints has two causes, and only one of them is addressed by a change of edge specification. Corrosion mechanisms and their control are described by NACE International, and winter treatment practice by the Federal Highway Administration.
Field evidence to collect
The diagnosis relies on comparing the edge with the route, and both sides of that comparison need a record. The table below lists what is worth collecting and what question each item answers.
| Evidence | What it answers |
|---|---|
| Contact-face measurement at several positions along the edge | Whether the loss is uniform or banded |
| A photograph of the edge next to a photograph of the route surface | Whether the wear positions line up with the polished sections |
| The number of passes and treatment applications per storm | How much sliding contact the edge has accumulated |
| Blade angle and down-pressure settings as run | Whether the edge was set for cutting or for clearing |
| Insert or edge height against the design minimum | Whether the geometry still supports cutting at all |
The second item is the one that settles most arguments and costs nothing to produce. Two photographs taken on the same day, one of the edge and one of the surface it has been working, are difficult to argue with and easy to keep with the fleet’s route records.
Which damage is permanent and which is not
Not all of the damage is permanent, and separating the recoverable from the rest prevents both premature replacement and false economy. Loss of material along the contact face is recoverable to the extent that the profile can be restored on a thick section, which returns a cutting geometry for a period rather than permanently.
Three conditions are not recoverable at reasonable cost: a wear flat that has reached the minimum section of the edge, a mounting line that has moved so the cutting angle can no longer be set, and deformation that has rolled the contact face rather than removing material. Where any of those is present, the edge has lost the geometry that made it cut and restoring it is a replacement decision rather than a repair. Measuring before deciding is what keeps that judgement factual, and the measurement routine is described on the blade wear measurement page.
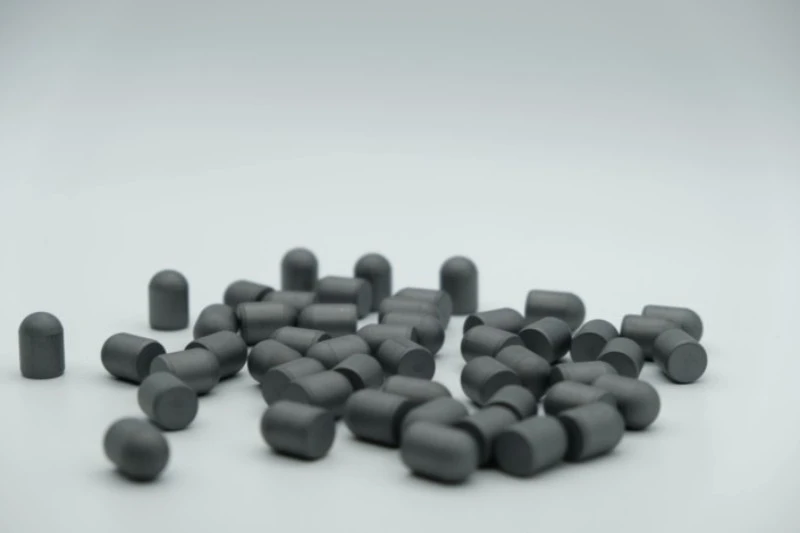
SENTHAI manufactures packed ice carbide kits and plow edges in Rayong, Thailand, with the insert arrangement and edge geometry confirmed against the surface a route presents. Test methods for the materials involved are published by ASTM International, winter maintenance research by the Transportation Research Board, and network-level practice by the Federal Highway Administration. Edges that need their wear pattern read against the route can be reviewed through the contact page.
FAQ
Does packed ice really damage a blade, or does it just not cut it?
Both, and the second causes the first. An edge that cannot cut rides the surface instead, and riding produces the damage: wear concentrated along the contact face, flats that stop it cutting even on looser material later, and impact damage when the blade drops into a gap it was riding over.
Why does my blade wear in the middle and not at the ends?
A wear pattern concentrated in the middle usually reflects where the surface is polished hardest rather than where the blade is weakest. Traffic compresses snow most heavily in the wheel tracks, so those sections polish first and the edge that rides them wears fastest along the same band.
Is salt making the edge wear faster?
Salt changes the material the edge meets more than it changes the edge itself. By lowering the freezing point it produces repeated partial melt and refreeze, which leaves a hard, smooth layer on the surface and a wet, corrosive environment around the blade. Both effects matter, and they act on different parts of the assembly.
Can a worn edge that has been polishing hardpack be recovered?
Partially. Where the loss is a wear flat on a thick edge, restoring the profile can bring back the cutting geometry for a time. Where the flat has developed on a thin edge or the mounting line has moved, the geometry that made it cut is gone and the recovery does not hold.
How do I prove hardpack is the cause rather than the material?
Compare where the wear sits along the edge with where the surface is polished. Where the two line up, the surface is driving the wear. Where the wear concentrates at the ends or beside fixings, the cause is mechanical. That comparison needs two measurements and settles the question before a supplier becomes involved.
Send the contact-face measurements, the route description and photographs of the surface as it stands after a freeze-thaw cycle. The SENTHAI engineering desk will confirm whether the edge geometry or the surface treatment is the limiting factor.
This article is one step in the Packed Ice Edge Guide, which explains why a standard edge skates across hardpack and how to set one up so it bites.