Three tests, not one, decide whether a custom edge is ready for production: a dimensional report, a fitment trial on a real machine, and a field trial long enough to expose the wear pattern.
Skipping any of them moves the discovery to the batch, where the cost is counted in scrapped pieces and lost weeks rather than in one more sample. The sequence below is the order that keeps each test meaningful.
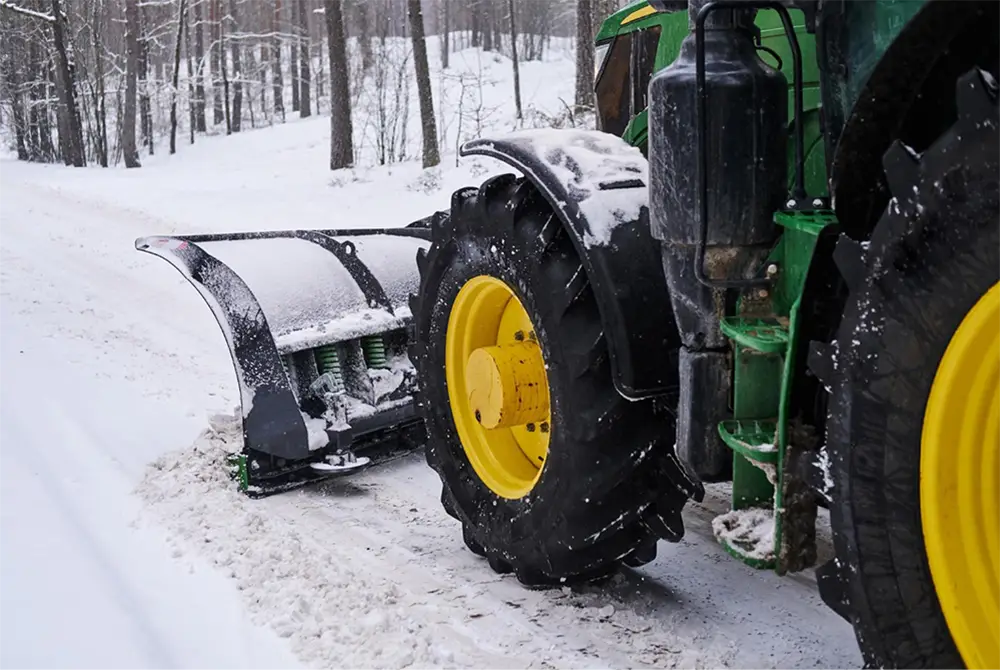
What a pre production sample plow edge has to prove
A sample proves the process, not the craftsman.
It has to show the dimensions within tolerance, the bolt layout fitting the machine, the join surviving the intended load, and the marking and packaging matching what the order will carry.
A hand-finished sample proves none of that reliably, because it was made outside the process the batch will use. The useful sample is the first piece of a small run, made with the same tooling, the same grade and the same inspection as the production order, and documented the same way. If the supplier cannot say which process the sample was made on, the sample has no predictive value.
For a custom edge, the acceptance criteria should be written before the sample is made. That is what turns the sample from a demonstration into an approval, and it is the document the first batch is later measured against.
What a sample cannot prove
A sample cannot prove wear life, and confusing the two is the most common way a sampling programme disappoints.
Wear depends on the surface, the down pressure, the speed and the season, none of which a laboratory can reproduce. A sample can prove that the geometry and the join are correct and that the material is what the specification calls for; the wear rate only appears after the edge has run on a route for weeks.
That is why the approval has two parts. The dimensional and process approval can be signed quickly against a written specification, while the field trial runs in parallel and either confirms the choice or sends one parameter back for revision. Treating them as one gate is what makes buyers wait a whole year for an approval that could have been split.
Documentation to accompany samples
The sample should arrive with the same document set the batch will carry, because the documents are part of what is being approved.
At minimum, that means the drawing revision the sample was made to, a dimensional record for the dimensions named in the specification, a material declaration with the standards the values were measured to, the result of the inspection applied to the joining step, and a batch reference that ties the piece to its production record. Where the buyer supplied the drawing, the sample should quote it back with its revision number so a later change cannot be mistaken for a tolerance failure.
Geometric dimensioning conventions for the drawing itself come from standards published by the American Society of Mechanical Engineers, and material test methods from ASTM International. The document set SENTHAI releases with a sample and a lot is described on the quality control page.
Fitment trial on a real vehicle
The fitment trial is the first test that catches problems no drawing can, and it takes an hour rather than a week.
It should be run on the machine the edge is intended for, with the machine on level ground and the existing hardware reused where the order will reuse it. The steps matter because a fitment fault can hide behind a loose fastening.
- Mount the edge with the specified bolts and torque, without forcing any hole.
- Check the hole alignment and record any hole that needed persuasion.
- Measure the protrusion and the clearances at both ends and at the centre.
- Raise and lower the plow through its full travel and watch for contact or interference.
- Record the result against the acceptance criteria before removing the edge.
A layout that only fits when the bolts are pulled up hard is not a fit, and it will show up later as a cracked edge or a loosened insert. Fleet fitment conventions are published by bodies such as the American Association of State Highway and Transportation Officials and equipment standards by SAE International, which is where the expected bolt layouts and edge profiles originate.
Field trial duration and conditions
The field trial should run until the edge has seen the conditions it was specified for, which for a winter part means conditions rather than a calendar.
A trial measured in weeks proves very little on a mild route, and a trial that runs through a single snow event proves almost nothing about abrasive wear. What the buyer should define up front is the service the edge has to see: hours of operation, surface type, plow speed and the down pressure the machine runs at. When those have been met, the trial has produced evidence.
The practical compromise is to start the field trial and the fitment approval at the same time. The dimensional and process approval releases the tooling and the material order; the field trial confirms the grade choice and either accepts it or sends one parameter back. Research on winter maintenance practice is published by the Transportation Research Board and the sector body, the Snow and Ice Management Association.
Recording results against criteria
Results become an approval only when they are recorded against the criteria that were fixed before the sample was made.
The record should carry the measured values rather than a pass word, because the values are what a later batch is compared with. Two dimensions in particular deserve their numbers written down: the ones with the tightest tolerance, and the ones that most affect fitment.
| Item | Record | Acceptance basis |
|---|---|---|
| Edge dimensions | Actual measurements, not a pass or fail flag | Drawing revision with stated tolerances |
| Bolt layout | Alignment result per hole after fitting | Fits without forcing, hardware reused |
| Protrusion and clearance | Measured at both ends and at the centre | Approved range for the machine and surface |
| Join inspection | Inspection result for the joining step | Agreed method and acceptance range |
| Marking and packaging | Photograph of the piece and the carton | Agreed branding and packing specification |
The photograph is worth more than it appears. Marking and packaging are the two things that change most easily between a sample and a batch, and a dated photograph settles the question without a rework.
Approval and sign-off records
The sign-off converts the sample into the specification, and it should be one page rather than a correspondence trail.
A usable record names the drawing revision, the grade and the joining method approved, the measured values from the trial, the person who approved them and the date. It should also state the scope: which sizes, which machine or range, and which packaging the approval covers. Without the scope, the first adjacent size becomes an argument.
Two practical rules keep the record useful. First, the approval belongs to a revision, so any later change to the drawing invalidates it rather than editing it. Second, the supplier should hold the same document and be able to quote its revision number on a delivery document, which turns goods-in into a comparison rather than an inspection.
Handling requested changes
Changes requested after the sample are normal, and the sequence below keeps them from turning into a second, unapproved product.
A change to the profile, the material or the join is a new revision rather than a tweak, and it needs its own first article. A change to the marking or the packaging usually needs only a photograph and a confirmation, since neither affects fitment or wear. Deciding which category a requested change falls into is the buyer’s job, and doing it at the time of the request prevents the most common failure in a custom programme: a batch that quietly carries a change nobody approved.
- Record the request with the reason and the date.
- Classify it as a specification change or a packaging change.
- For a specification change, issue a new revision and require a first article.
- For a cosmetic change, confirm against a sample or a photograph.
- Re-issue the approval record with the new revision before the next order.
The fifth step is the one that gets skipped when the change is small, and it is exactly the case where a later dispute becomes unresolvable, because nobody can say which version was approved. The production side of that process is described on the factory page.
FAQ
How long does sample approval normally take?
Allow a week or two for the sample to be made and shipped, a day for the fitment trial, and a full operating period for the field trial, which in a seasonal product usually means waiting for conditions rather than for the part.
Who should sign the approval record?
The person who carries the consequence if the batch is wrong. In practice that is normally the buyer’s engineering or quality function, even when the trial was run by an operator or a dealer, because the signature is what converts a sample into a production specification.
What happens if the sample passes but the first batch does not?
The approval record is the reference, so the first batch is checked against it rather than against memory. A difference in the join, the marking or the dimensions is a deviation from the approved sample, and it is treated as a non-conformance rather than as an acceptable variation.
Send the drawing or the measured layout and the machine the edge has to fit. SENTHAI will produce a sample from the production process, with the dimensional record and the join inspection that the approval is signed against.
This article is one step in the Sourcing Carbide Wear Parts Guide, which covers the technical pack, supplier selection, landed cost and supply risk.